
7 Tips for Automatic Die Cutting and Creasing Machines
An Automatic Die Cutting And Creasing Machine can transform flat sheets into accurate packaging components. Its performance depends on more than speed. Material choice, tooling quality, pressure control, and operator judgment all influence the final result.
In practical production, small details often create large differences. A slightly misaligned crease may cause cartons to fold unevenly. Excessive pressure can damage delicate paperboard and shorten die life. These machines also respond differently to coated stock, corrugated board, and laminated sheets. Understanding those differences helps operators build safer, more consistent workflows.
No setup is perfect.
This guide presents seven useful tips for improving daily performance. It covers die and matrix selection, sheet positioning, pressure adjustment, feeding stability, waste removal, routine inspection, and operator training. Each point connects technical knowledge with realistic production conditions, including dust near the feed table and uneven stacks after long runs.
Experienced teams still make mistakes. A rushed setup may pass the first inspection but create defects later. That is why measured testing, documented settings, and regular maintenance remain essential. Operators should check registration, crease depth, cutting quality, and finished dimensions before increasing machine speed.
The goal is not simply to run faster. It is to achieve repeatable results while protecting materials, tooling, and people. Some recommendations may require adjustment for your equipment. That reflection matters, because every production environment has different demands, limitations, and learning points.
Understanding Automatic Die Cutting and Creasing Machine Functions
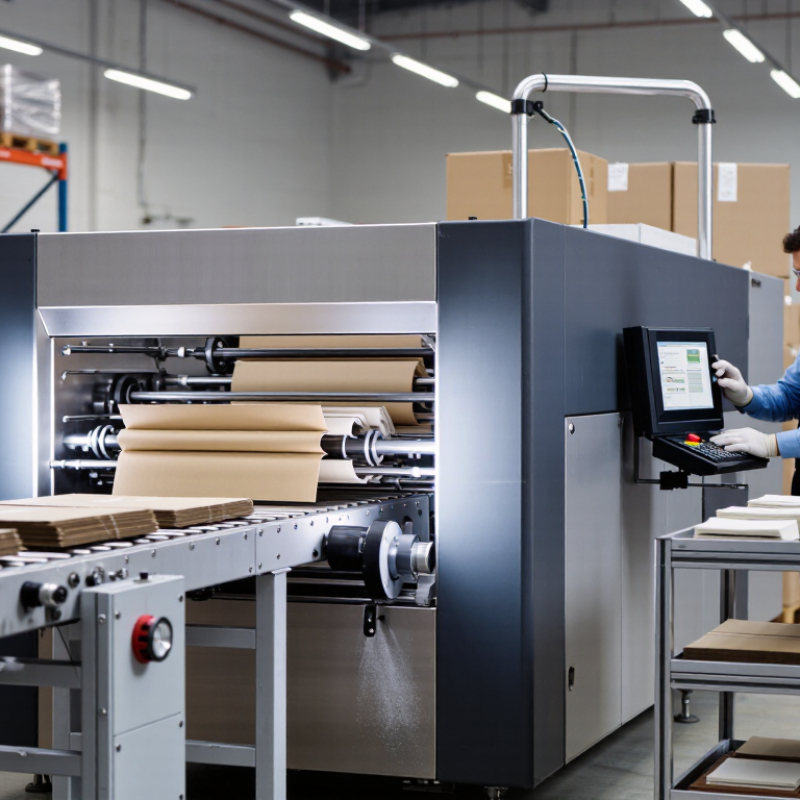
Automatic Die Cutting And Creasing Machines do more than press sheets through a cutting station. They coordinate feeding, registration, die cutting, creasing, stripping, and delivery. Understanding this sequence helps operators control quality and reduce waste. Start with stable feeding. Check pile height, suction timing, and sheet separation before production begins. A small feeding error can become a visible cutting shift.
Accurate registration depends on clean sensors, correct side-lay settings, and consistent sheet dimensions. Test several sheets before increasing speed. The die applies pressure, while the creasing section forms controlled folding lines. Excessive pressure may damage fibers or create unwanted marks. Insufficient pressure can produce weak folds. I have learned that a perfect setting on paper can still fail with humid stock. That assumption needs review.
Choose the die and matrix according to material thickness and fold direction. Inspect cutting edges and creasing rules for wear. Worn tooling often causes rough corners and uneven folds. Keep the stripping station properly aligned, especially when small waste pieces surround the product. The delivery unit should stack sheets evenly without disturbing fresh creases. Operators also need to monitor noise, vibration, and temperature during long runs. These details often reveal mechanical problems early. Record speed, pressure, material, and results for repeat jobs. Practical records are useful, although they are not always complete. Never adjust moving parts casually. Follow the machine’s safety procedures and isolate power before maintenance.
7 Tips for Automatic Die Cutting and Creasing Machines - Understanding Automatic Die Cutting and Creasing Machine Functions
| No. | Function or Tip | How It Works | Typical Materials or Range | Practical Operating Tip | Main Result |
|---|---|---|---|---|---|
| 1 | Confirm Material Compatibility | The feeder and platen section transport sheets to a cutting and creasing die. Correct pressure and die selection depend on the material structure. | Paperboard, folding carton stock, corrugated sheets, synthetic sheets, and other die-cuttable sheet materials. | Check sheet thickness, grain direction, coating, moisture, and surface condition before production. Use a sample sheet for testing. | Fewer cracks, tears, feeding problems, and inaccurate folds. |
| 2 | Set the Automatic Feeder Correctly | A pile feeder separates sheets and delivers them into the machine at a controlled speed and spacing. | Flat sheets with consistent dimensions and properly aligned stacks. | Adjust pile height, side guides, front guides, suction, and sheet separation. Keep the stack level and avoid excessive air or pressure. | Stable sheet flow and reduced double-sheet or skewing errors. |
| 3 | Use Register and Alignment Controls | Front lays, side lays, sensors, and control settings position each sheet against the die before the pressing cycle. | Printed cartons, labels, folders, presentation packaging, and multi-up layouts. | Use a printed registration mark or a fixed reference edge when applicable. Inspect the first sheets for image-to-cut alignment. | Consistent cutting position and reduced material waste. |
| 4 | Balance Die-Cutting Pressure | The platen applies pressure to force cutting rules through the sheet while the die board maintains the required pattern. | Cutting pressure varies with material thickness, density, rule height, cutting area, and die condition. | Increase pressure gradually from a low setting. Use make-ready sheets to correct local pressure instead of overloading the entire platen. | Clean cuts, longer die life, and less crushing of the sheet. |
| 5 | Optimize Creasing Quality | Creasing rules press controlled channels into the sheet, creating fold lines without completely cutting through the material. | Folding carton board, coated paperboard, cards, folders, and packaging blanks. | Match crease channel width and rule height to the board thickness and fiber direction. Test both mountain and valley folds. | Sharper folds with less cracking, whitening, and spring-back. |
| 6 | Adjust Stripping and Delivery | Stripping tools remove waste from around the cut blanks, while the delivery section separates and stacks finished sheets. | Carton blanks, labels, tags, inserts, and complex layouts with internal waste. | Use properly positioned stripping pins and check that waste exits freely. Adjust delivery jogging to prevent uneven stacks. | Cleaner blanks, faster finishing, and fewer delivery stoppages. |
| 7 | Follow Safety and Maintenance Checks | Interlocks, guards, emergency stops, lubrication points, sensors, and inspection routines help protect operators and maintain machine accuracy. | Applicable to every automatic die cutting and creasing production run. | Stop the machine before entering guarded areas. Inspect cutting plates, grippers, belts, sensors, lubrication, and die fasteners according to the operating manual. | Safer operation, stable quality, and reduced unplanned downtime. |
Note: Operating settings vary according to machine design, die construction, sheet material, and job specifications. Always verify final settings with the machine manufacturer's operating instructions and a production sample.